Differential - Setting Rear Axle Pinion Depth
88chevy27Number: 88-322-4B
Section: 4B
Date: AUGUST, 1988
Subject: SERVICE MANUAL UPDATE: SETTING REAR AXLE PINION DEPTH
Model and Year: 1987-88 CAMARO
TO: ALL CHEVROLET DEALERS
Service manual instructions have been changed to enable the technician to accurately calculate the thickness of the shim pack used to determine the proper depth of the rear axle drive pinion.
The new sheet replaces the 1987 and 1988 Service Manual information published in the 1987-88 Camaro service manuals.
Replace the original service manual instructions in Section 4B with the ones supplied in this bulletin.
FIGURE 1 - PINION GAGE PLATE INSTALLED IN CARRIER:
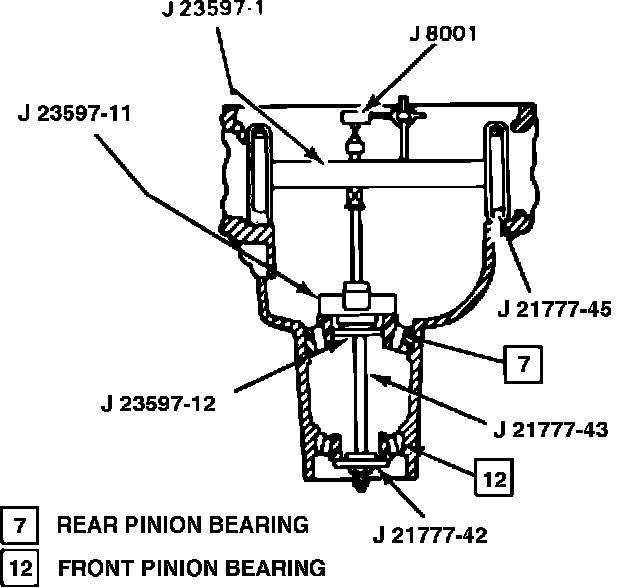
FIGURE 2 - CHECKING PINION DEPTH:
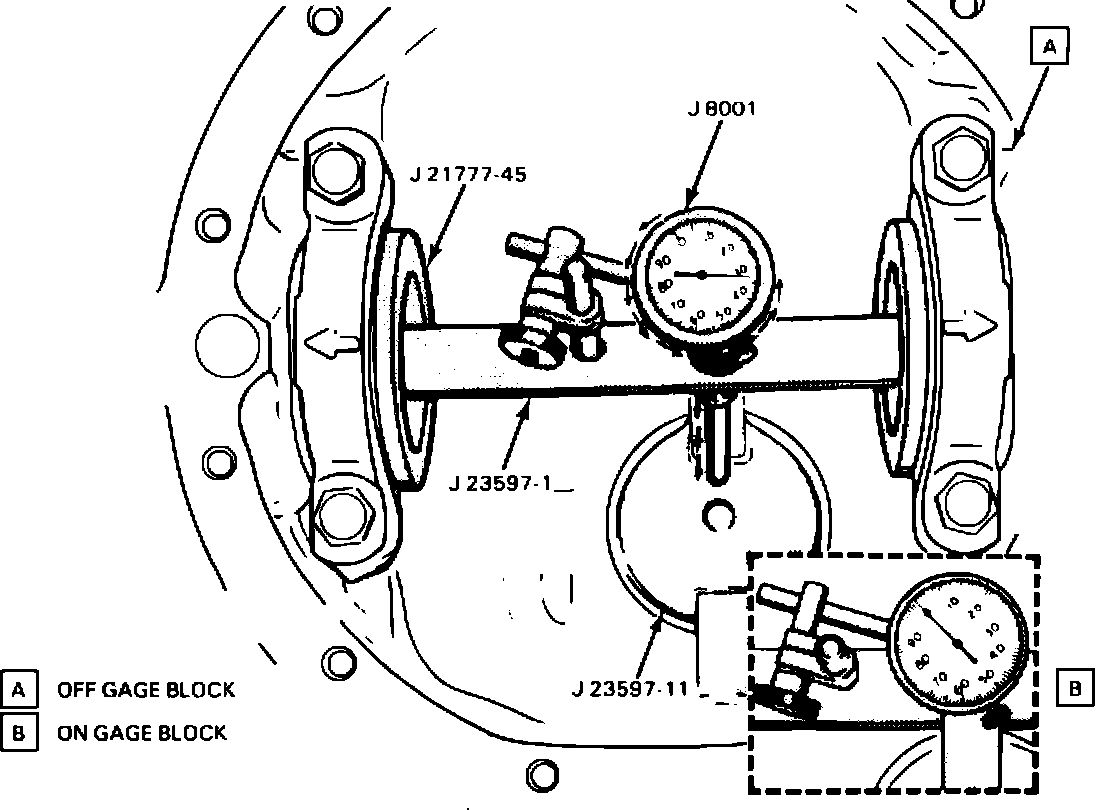
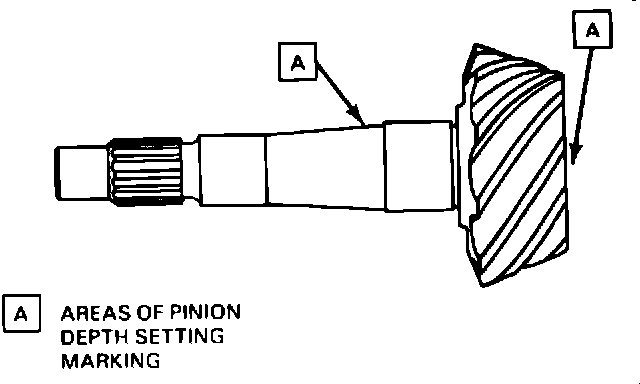
FIGURE 3 - PINION MARKING:
PINION DEPTH
Figures 1 through 3
Tools Required:
Camaro
* J 8001 Dial Indicator Set
* J 23597-1 Arbor, 7-1/2-inch and 7-5/8-inch Ring Gears
* J 23597-11 Gage Plate, 7-1/2-inch and 7 5/8-inch Ring Gears
* J 23597-12 Rear Pilot Washer, 7-5/8-inch Ring Gear J 21777-1 Arbor, 8-1/2-inch Ring Gear J 21777-29 Gage Plate, 8-1/2-inch Ring Gear J 21777-35 Rear Pilot Washer, 8-1/2-inch Ring Gear J 21777-40 Rear Pilot Washer, 7-1/2-inch Ring Gear
* J 21777-42 Front Pilot Washer
* J 21777-43 Stud Assembly, Bolt
* J 21777-45 Side Bearing Discs
Pinion depth is measured with a pinion setting gage. The gage provides a "nominal" or "zero" pinion as a gaging reference.
vClean
1. All parts of gage.
2. Side bearing bore.
3. Front and rear bearing cups.
^ Lubricate front pinion bearing (12) and rear pinion bearings (7) with rear axle lubricant.
vInstall or Connect
1. J 21777-43 through J 23597-12, as required. Refer to Figure 1.
2. J 23597-11 or J 21777-29.
3. J 21777-42 and nut in carrier.
vTighten
^ Nut to 2.3 N-m (20 in.lbs.).
^ Rotate J23597-11 or J21777-29 to seat the bearings.
^ Mount J8001 on J23597-1 or J21777-1 and preload indicator against plunger about 1.27 mm (0.050 inch).
4. J 21777-45 on J 23597-1 or J 21777-1 and position unit in carrier.
5. Side bearing caps and bearing cap bolts.
vTighten
^ Bearing cap bolts to 75 N-m (55 ft.lbs.).
vMeasure
^ Pinion depth.
^ Rotate J 23597-1 or J 21777-1 slowly back and forth until J 8001 reads the greatest deflection (the point where the needle changes direction). At that point, set J 8001 to zero. Repeat rock action to verify the zero setting.
^ After zero setting is obtained, rotate J 23597-1 or J21777-1 just until the plunger no longer touches J 23597-11 or J 21777-29. This provides the gaging reference of a "nominal" or "zero" pinion.
^ Record J 8001 reading at pointer position. This indicates the proper shim to use.
Example: if pointer moved counterclockwise 1.70 mm (0.067 inch) to a dial reading of 0.84 mm (0.033 inch), this indicates a shim thickness of 0.84 mm (0.033 inch) (Figure 2).
^ On 7-1/2-inch and 7 5/8-inch ring gear axle assemblies (Type K), select the correct drive pinion shim to be used during reassembly on the following basis:
- No marking on drive pinion, correct shim has thickness EQUAL to J 8001 reading.
- Plus (+) marking on drive pinion, shim thickness indicated by J 8001 INCREASES by the amount on the drive pinion.
- Minus (-) on drive pinion, shim thickness indicated by J 8001 DECREASES by the amount on the drive pinion.
^ On 8-1/2-inch ring gear axle assemblies (Type G) drive pinions are nominal gears and do not have markings. Required shim thickness is EQUAL to J 8001 reading.
^ Shims are available in 0.03 mm to 0.94 mm (0.050 inch to 0.037 inch). Shim thickness is etched on the flat surface for easy identification.
vRemove or Disconnect
^ Loosen J 21777-43 and remove special tools and both bearings from carrier.
vInstall or Connect
1. Correct shim on drive pinion.
2. Drive pinion rear bearing (7).
vAssemble
^ Differential case. Refer to "Differential Case Removal with Axle Shafts Removed," in the appropriate service manual.
vMeasure
^ Preload of the total assembly at the pinion yoke nut. With new bearings, preload is 4.0 to 4.5 N-m (35 to 40 in.lbs.) rotating torque with a new seal. With used bearings, preload is 2.3 to 2.8 N-m (20 to 25 in.lbs.) rotating torque with a new seal.